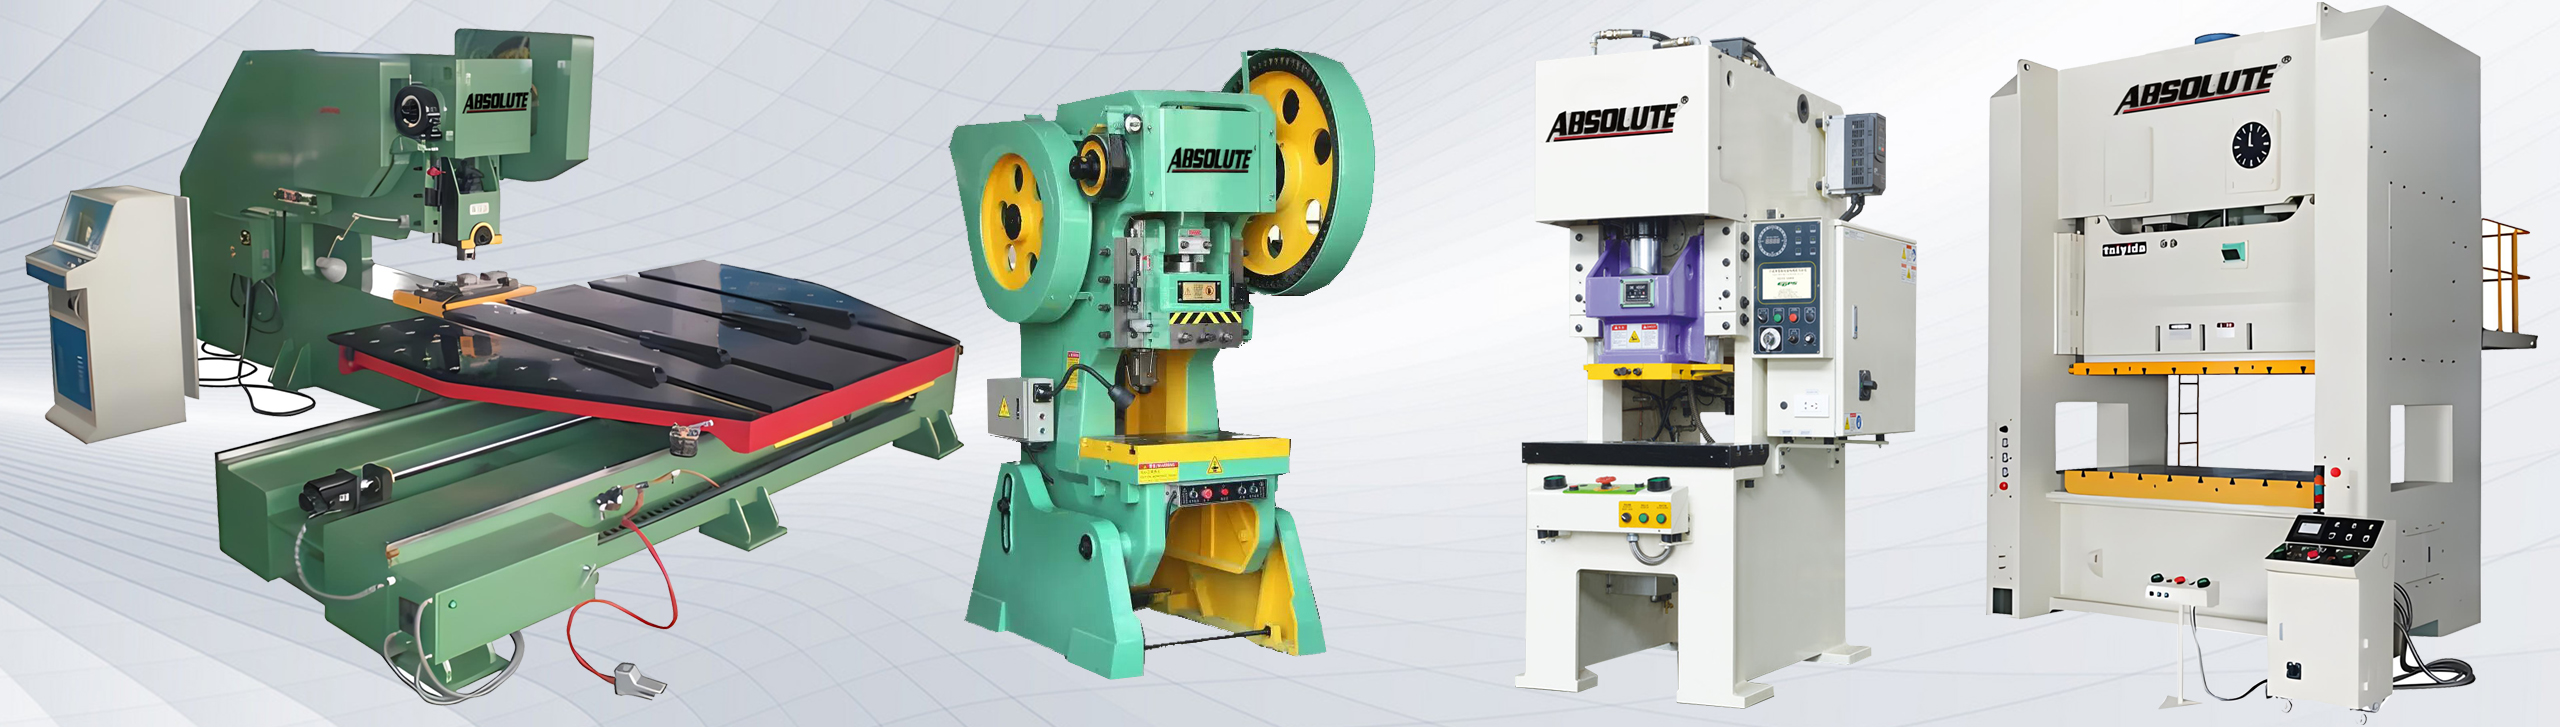
Compare pneumatic and mechanical punch presses for sheet metal stamping. Send your part drawings, material, thickness and required operations to discuss machine and tooling selection.
Pneumatic or mechanical clutch punch press: match the press to the die
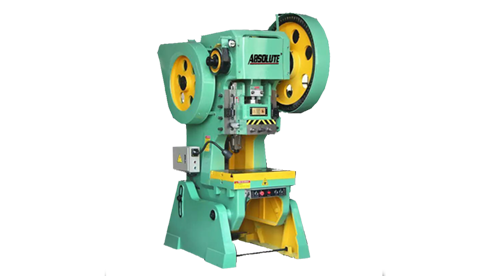
For crank-driven stamping equipment, a pneumatic punch press often refers to an air-operated clutch and brake, not an air cylinder that supplies punching force. Both types can use a motor, flywheel and crank mechanism. Confirm the quoted drive, clutch and brake arrangement, then compare it against the part drawing and die.
Questions to ask when comparing clutch and brake configurations
Requirement
Pneumatic clutch/brake
Mechanical clutch
Power transmission
Air engages or controls the clutch/brake. Verify the mechanical drive and its force and energy limits.
A mechanical engagement connects the drive to the slide. Verify the exact clutch design and operating limits.
Cycle control
Confirm clutch/brake control, permitted stopping positions, cycling mode and the specified air supply.
Confirm whether it is a full-revolution or other design, its cycle behavior and safeguarding requirements.
Tooling compatibility
Check rated force position, stroke, shut height, table and slide dimensions against the die.
Check the same dimensions and force position, together with the clutch's operating limitations.
Prepare these details for a quotation
Material grade, thickness range, part drawing and the punching, blanking or forming operation.
Die dimensions, die height, guide arrangement, required shut height and working clearance.
Required force, stroke, strokes per minute or production target, and feeding method.
Required clutch/brake type and cycling mode; for air-operated systems, available air pressure, flow and air quality.
Destination country, electrical supply, guarding, workshop space and installation requirements.
Common punch press buying questions
Does air pressure determine the stamping tonnage?
For a mechanically driven press with a pneumatic clutch, the compressed air operates the clutch/brake system. It does not make the press an air-cylinder stamping machine. The rated force, working position and available flywheel energy remain mechanical machine specifications. Confirm those specifications separately from the air supply requirement.
Does rated tonnage equal usable force at every point?
No. Crank-driven presses are commonly rated at a stated position near bottom dead center. Working force and energy limits must suit the die's operation throughout the cycle. Material, cut perimeter and die clearance affect the required force. Check the working point and die requirements with the supplier.
What information helps avoid an unsuitable die space?
Provide die length and width, die height, guide posts, shut height, slide dimensions and the required opening. Include the feed direction and any part ejection or scrap removal. A press can have enough nominal force yet lack the table, stroke or daylight needed for the tooling.
Use the punching force calculator for a preliminary estimate, then send the part and die drawings. Force calculations do not replace a tooling, guarding and installation review.