Absolute Cnc Machine Co., Ltd.     Mobile/WhatsApp:+86 13115000086     E-mail:info@cnabsolute.com

Your location:Home>>Products>>Rolling Machine

3-Roll & 4-Roll Plate Rolling Machines

Explore 3-roll and 4-roll plate rolling machines for metal forming. Share material grade, plate thickness and width, target diameter and part drawings to discuss a suitable configuration.

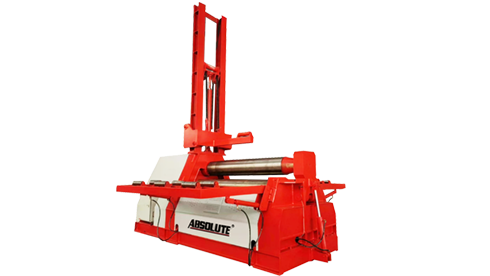
Four-Roller Hydraulic Metal Sheet Rolling Machine

Four-Roller Hydraulic Metal Sheet Rolling Machine

This machine is a hydraulic four-roller bending machine and used to do pre-bending the end of plate, rolling it into round, cone and other shapes. Four roller bending machine is recognized as the fastest, most accurate, most likely to use the machine.The rest of the straight edge segment is greatly reduced-only one end of the board is fed. There is also the source of its outstanding pre bending capacity: clip point completely fell on the edge of the plate.Automatic feeding material-with the feed side of the opposite side of the rear roll, can be used as a rear stop material, the plate immediately into a right angle parallel position, sheet metal flat easy, single operation can.After the correction of the plate, the upper and lower parts of the middle of the clip to the middle of the clamp, so it is safe and easy to operate, there is no risk of sheet slippage.In the front of the plate, the diameter of the cylinder can be made immediately. Because only in the machine tool side need to enter the space can be used, which means that the operation of the machine tool is less space.After the cylinder volume is made, the end of the roll is made. A cylinder by bending forming.Taper coil is easy, can be rolled to the biggest angle of 30 degree cone. The side roll is inclined to determine the angle of the cone, and the center of the lower center can also tilt, clamp and drive plate.In the rolling process, ensure the plate clamping and driving, four roller bending machine is the single most applicable on the NC and CNC systems through effective control of the bending machine.In the cylinder after rolling, rolling on the tail edge (four roller bending machine can bend ahead, can also bend back). A cylinder by bending forming.

MORE

Plate rolling machine selection guide

3-roll or 4-roll plate rolling machine: compare the forming workflow

Choose a plate roll from the parts you need to form, including material grade, thickness, width, finished diameter and cone requirements. A machine's nominal capacity is only a starting reference. Pre-bending length, roll arrangement, minimum diameter, support and handling influence the finished cylinder and the time needed for each setup.

Questions to ask when comparing 3-roll and 4-roll machines
Requirement3-roll machine4-roll machine
Loading and alignmentReview how the plate is inserted, aligned and repositioned during forming. The operator's setup method matters.The additional roll can support a workflow with controlled clamping and alignment; confirm the actual sequence on the quoted model.
Edge pre-bendingAsk how the required edge pre-bending is achieved and how much handling is needed for your diameter range.Review whether the roll arrangement supports the pre-bending sequence required for your part and operator method.
Production mixCompare changeover steps, cone forming options and operator access for your batch sizes.Compare setup repeatability, plate handling and controls for the parts you make most often.

Send these details for a useful quotation

Common plate rolling machine buying questions

Is a 4-roll machine always faster?

It can simplify alignment and clamping for some workflows, but the result depends on the part, operator sequence, tooling and handling equipment. A 3-roll machine may suit a different mix of diameters and production volumes. Compare a complete cycle using your drawing rather than a general speed claim.

What is the minimum diameter I can roll?

Minimum diameter depends on roll diameters, machine geometry, material properties, thickness and the required pre-bend. It is not determined by plate width alone. Ask for a confirmed range using your material and thickness, and provide a sample drawing for review.

Can the same machine form cones?

Some configurations include provisions for cone forming, but the usable range depends on the roll arrangement, controls, support and the cone dimensions. State the smallest and largest cone you need, including angle and plate details, before requesting a quotation.

Use the roll bending force calculator for an initial estimate, then send the cylinder or cone drawing so the roll geometry and forming sequence can be reviewed.

Send a rolling drawing for quotation
Request a quoteWhatsApp